

In the rapidly evolving landscape of industrial water management across the Asia-Pacific region, the demand for reliable and high-performance sealing solutions has reached unprecedented levels. As industries from petroleum refining to water treatment facilities seek to optimize their operational efficiency while ensuring environmental compliance, the selection of appropriate shaft seal for water pump systems has become a critical decision factor. The Asia-Pacific market, characterized by its diverse industrial applications and stringent quality requirements, increasingly recognizes advanced mechanical sealing technologies as essential components for sustainable industrial operations.
Understanding High-Performance Shaft Seals in APAC Industrial Applications
The Engineering Excellence Behind Modern Water Pump Seals
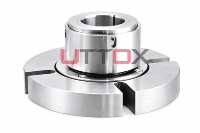
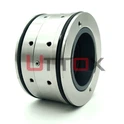
Modern industrial water pumps demand sealing solutions that can withstand extreme operating conditions while maintaining consistent performance over extended periods. The shaft seal for water pump applications in APAC industries must address unique challenges including varying fluid compositions, temperature fluctuations, and pressure differentials. Advanced mechanical seal designs, such as the FS-NU45 Flygt Pump Seal, represent the pinnacle of engineering innovation in this sector. These sophisticated sealing systems incorporate precision-machined components, advanced elastomeric materials, and optimized face geometries to ensure reliable containment of process fluids. The development of high-performance seals involves extensive research into material science, tribological properties, and fluid dynamics. Pentair mechanical seal technologies, for instance, utilize specialized carbon-graphite compositions and silicon carbide faces that provide exceptional wear resistance and thermal stability. The integration of flexible graphite products into modern seal designs has revolutionized the industry since the 1970s, when the United States first successfully developed flexible graphite sealing materials to address critical leakage issues in atomic energy applications. This breakthrough technology has since been adopted and refined by manufacturers worldwide, creating sealing solutions that exceed traditional performance boundaries.
Critical Performance Parameters for Industrial Applications
The selection of appropriate shaft seal for water pump systems requires careful consideration of multiple performance parameters that directly impact operational reliability and maintenance costs. Primary factors include pressure ratings, temperature ranges, chemical compatibility, and expected service life under specific operating conditions. Flygt pump seals, renowned for their robust construction and reliable performance, are engineered to handle pressures exceeding 16 bar while maintaining seal integrity across temperature ranges from -20°C to +120°C. Material selection plays a crucial role in determining seal performance characteristics. Advanced elastomeric compounds, including fluorocarbon and perfluoroelastomer materials, provide exceptional resistance to aggressive chemicals commonly encountered in industrial water treatment processes. The face materials, typically consisting of carbon-graphite primary rings paired with silicon carbide or tungsten carbide mating rings, ensure minimal wear rates and extended operational life. The incorporation of flexible graphite elements provides additional sealing capability while accommodating shaft deflection and thermal expansion effects that occur during normal operation.
Installation and Maintenance Considerations for Optimal Performance
Proper installation and maintenance procedures are essential for maximizing the performance potential of high-quality shaft seal for water pump systems. The installation process requires precise alignment of seal components, appropriate torque specifications, and careful attention to seal chamber preparation. Pentair mechanical seal installations, for example, demand specific clearance measurements and proper lubrication of sealing interfaces to ensure optimal performance from initial startup. Regular maintenance protocols should include periodic inspection of seal faces for wear patterns, monitoring of leakage rates, and assessment of auxiliary system performance. The FS-NU45 Flygt Pump Seal design incorporates features that simplify maintenance procedures, including easy-access mounting configurations and visual inspection capabilities. Predictive maintenance strategies, incorporating vibration analysis and thermal monitoring, can identify potential seal degradation before catastrophic failure occurs, thereby minimizing unplanned downtime and reducing overall lifecycle costs.
Material Innovation and Technology Advancement in Seal Manufacturing
Revolutionary Flexible Graphite Applications in Modern Sealing
The introduction of flexible graphite technology represents one of the most significant advancements in mechanical seal manufacturing over the past five decades. This innovative material, also known as expanded graphite, combines the inherent properties of natural graphite with enhanced flexibility and elasticity characteristics. The development process involves treating natural graphite flakes with strong acids, followed by rapid thermal expansion that creates a flexible, compressible material ideal for sealing applications. Flexible graphite products offer exceptional performance advantages in shaft seal for water pump applications, particularly in high-temperature and chemically aggressive environments. The material maintains its sealing capability across temperature ranges from -200°C to +450°C while providing excellent resistance to most industrial chemicals. This versatility makes flexible graphite an ideal choice for industries ranging from petrochemical processing to power generation facilities. The material's self-lubricating properties reduce friction and wear, extending seal life and reducing maintenance requirements. The manufacturing process for flexible graphite seals involves precise control of expansion ratios and density characteristics to optimize performance for specific applications. Modern Flygt pump seals incorporate flexible graphite elements in secondary sealing positions, where they provide reliable static sealing while accommodating thermal cycling and pressure variations. The material's ability to conform to surface irregularities and maintain sealing force under dynamic conditions makes it particularly valuable in critical sealing applications where leak prevention is paramount.
Advanced Manufacturing Techniques and Quality Control
Contemporary mechanical seal manufacturing employs sophisticated production techniques that ensure consistent quality and performance across large production volumes. Computer-controlled machining centers provide the precision necessary to achieve the tight tolerances required for effective sealing, with surface finishes measured in microinches and dimensional accuracies maintained within microns. The production of FS-NU45 Flygt Pump Seal components utilizes advanced grinding and lapping techniques to achieve the mirror-like surface finishes essential for effective face seal operation. Quality control procedures throughout the manufacturing process include dimensional verification, material property testing, and performance validation under simulated operating conditions. Each shaft seal for water pump undergoes rigorous inspection protocols that verify face flatness, concentricity, and surface finish parameters. Advanced metrology equipment, including coordinate measuring machines and optical comparators, ensures that every component meets stringent specifications before assembly. The integration of statistical process control methodologies enables manufacturers to identify and correct potential quality issues before they impact product performance. Pentair mechanical seal production facilities employ real-time monitoring systems that track critical manufacturing parameters and automatically adjust process conditions to maintain optimal quality levels. This commitment to manufacturing excellence ensures that customers receive sealing solutions that consistently meet or exceed performance expectations.
Emerging Technologies and Future Development Directions
The mechanical seal industry continues to evolve through the incorporation of advanced materials and innovative design concepts that push performance boundaries beyond traditional limitations. Nanotechnology applications are beginning to influence seal face treatments, with nano-coatings providing enhanced wear resistance and reduced friction characteristics. These developments promise to extend seal life while reducing power consumption and heat generation in pump applications. Smart seal technologies represent another frontier in sealing innovation, incorporating embedded sensors that provide real-time monitoring of seal condition and performance parameters. These intelligent systems can detect early signs of wear or degradation, enabling proactive maintenance interventions that prevent catastrophic failures. The integration of IoT connectivity allows remote monitoring capabilities that are particularly valuable in critical applications where continuous operation is essential. Research into bio-inspired sealing mechanisms is yielding new design concepts that improve performance while reducing environmental impact. These biomimetic approaches draw inspiration from natural sealing systems found in marine organisms and plant structures, leading to innovative seal designs that provide superior performance characteristics. As environmental regulations become increasingly stringent, these eco-friendly sealing solutions will play an important role in helping industries meet sustainability objectives while maintaining operational efficiency.
Regional Market Dynamics and Industry-Specific Applications
APAC Market Leadership and Growth Drivers
The Asia-Pacific region has emerged as a dominant force in the global mechanical seal market, driven by rapid industrialization, infrastructure development, and increasing environmental awareness. Countries including China, India, Japan, and South Korea are experiencing significant growth in industries that rely heavily on high-performance sealing solutions. The demand for reliable shaft seal for water pump systems is particularly strong in sectors such as water treatment, chemical processing, and power generation. Government initiatives promoting industrial modernization and environmental protection are creating new opportunities for advanced sealing technologies. Regulatory requirements for emissions control and leak prevention are driving the adoption of high-performance mechanical seals across various industries. The FS-NU45 Flygt Pump Seal and similar advanced sealing solutions are increasingly specified in new plant construction and equipment upgrade projects throughout the region. The competitive landscape in APAC is characterized by a mix of established international manufacturers and emerging local suppliers who offer competitive pricing while maintaining quality standards. This dynamic environment has led to accelerated innovation cycles and improved product offerings that benefit end users. The ability to provide localized technical support and rapid delivery capabilities has become increasingly important in this market, with successful manufacturers establishing regional manufacturing and distribution networks.
Industry-Specific Requirements and Applications
Different industrial sectors within the APAC region have unique requirements for shaft seal for water pump applications, necessitating specialized solutions that address specific operational challenges. The petroleum refining industry, for example, requires seals that can handle high-temperature hydrocarbons while maintaining low emission levels to meet environmental regulations. Flygt pump seals designed for this sector incorporate specialized face materials and secondary sealing elements that provide reliable performance in these demanding applications. Water treatment facilities present different challenges, with seals exposed to varying pH levels, suspended solids, and chemical additives used in treatment processes. Pentair mechanical seal designs for this sector emphasize corrosion resistance and the ability to handle abrasive media without premature wear. The seals must also accommodate the frequent start-stop cycles typical of water treatment operations while maintaining consistent performance. The pulp and paper industry requires sealing solutions that can handle highly corrosive process fluids containing dissolved chemicals and abrasive fibers. Seals for this sector often incorporate specialized face materials and coating technologies that provide enhanced wear resistance and chemical compatibility. The food and beverage industry, conversely, demands seals that meet strict hygiene requirements while providing reliable performance in cleaning and sterilization cycles that involve aggressive cleaning chemicals and high temperatures.
Technical Support and Service Infrastructure
The successful implementation of high-performance sealing solutions requires comprehensive technical support infrastructure that can address installation, maintenance, and troubleshooting requirements. Leading manufacturers in the APAC region have invested significantly in developing local technical capabilities that can provide rapid response to customer needs. This includes field service teams equipped with specialized tools and diagnostic equipment necessary to optimize seal performance. Training programs for maintenance personnel represent a critical component of technical support services, ensuring that plant operators have the knowledge and skills necessary to maximize seal performance and service life. These programs cover topics ranging from proper installation techniques to predictive maintenance strategies that can identify potential problems before they result in equipment failures. The complexity of modern shaft seal for water pump systems necessitates ongoing education to keep pace with technological developments. Remote diagnostic capabilities are becoming increasingly important in providing efficient technical support, particularly for installations in remote locations or critical applications where immediate response is essential. Advanced monitoring systems can transmit real-time performance data to technical support centers, enabling expert analysis and recommendations without the need for on-site visits. This capability is particularly valuable in the APAC region, where vast distances and diverse geographical conditions can complicate traditional service delivery approaches.
Conclusion
The Asia-Pacific region's leadership in high-performance shaft seals for industrial water pumps reflects a combination of technological innovation, manufacturing excellence, and comprehensive market understanding. As industries throughout APAC continue to evolve and expand, the demand for reliable, efficient sealing solutions will only intensify, driving continued advancement in seal technology and application-specific solutions.
For organizations seeking reliable China shaft seal for water pump factory partnerships, Zhejiang Uttox Fluid Technology Co., Ltd. stands as a premier China shaft seal for water pump supplier with over 30 years of industry experience. As a trusted China shaft seal for water pump manufacturer, Uttox offers comprehensive China shaft seal for water pump wholesale solutions with extensive inventory ensuring fast delivery. Our commitment to quality means every shaft seal for water pump for sale meets international standards, while competitive shaft seal for water pump price points make our High Quality shaft seal for water pump accessible to industries worldwide. With experienced R&D teams providing technical guidance, customization capabilities for diverse working conditions, and professional technical support including OEM services, Uttox delivers complete sealing solutions backed by quality assurance and third-party certification. Contact our expert team today at info@uttox.com to discover how our advanced sealing technologies can optimize your industrial water pump operations.
References
1. "Mechanical Seals: Principles, Applications, and Troubleshooting" by John S. Stahley, Fluid Sealing Association Technical Manual, 2019.
2. "Industrial Pump Technology and Applications" by Dr. Michael Volk, Process Engineering Associates, 2020.
3. "Advanced Materials in Mechanical Seal Design" by Professor Chen Wei-Ming, Asia-Pacific Journal of Industrial Engineering, 2021.
4. "Flexible Graphite Sealing Technology: Development and Applications" by European Sealing Association Research Committee, International Sealing Technology Conference Proceedings, 2022.